Prototype Molding remains a practical bridge between product design and repeatable manufacturing. It helps engineers test fit, texture, tolerances, and assembly before committing to expensive production tooling. The best manufacturers combine material knowledge, mold engineering, machining accuracy, and responsive project management.
Industry data supports this growing need. The Wohlers Report 2024 valued the global additive manufacturing industry at approximately $20.0 billion in 2023, reflecting stronger demand for faster product development and customized parts. Grand View Research also identifies rapid prototyping as an important application within advanced manufacturing, especially for automotive, medical, aerospace, and consumer products. These figures do not measure every molding project directly. However, they show the commercial pressure behind shorter development cycles.
This guide examines top Prototype Molding manufacturers worldwide through practical criteria. These include tooling capability, polymer selection, dimensional control, surface finishing, quality systems, and production scalability. Certifications such as ISO 9001 or IATF 16949 can support credibility, but certificates alone prove little. Real evidence matters more: inspection reports, sample parts, tolerance data, and clear communication during design changes.
Details matter.
A supplier may offer a low quotation while excluding mold maintenance, secondary operations, or shipping risks. Another manufacturer may appear expensive but reduce redesigns through early DFM feedback. No ranking is perfect. Supplier performance can vary by project complexity, region, and material requirements. Therefore, this overview focuses on verifiable capabilities rather than promotional claims, while recognizing that manufacturers and buyers must still validate results through samples, audits, and documented quality checks.
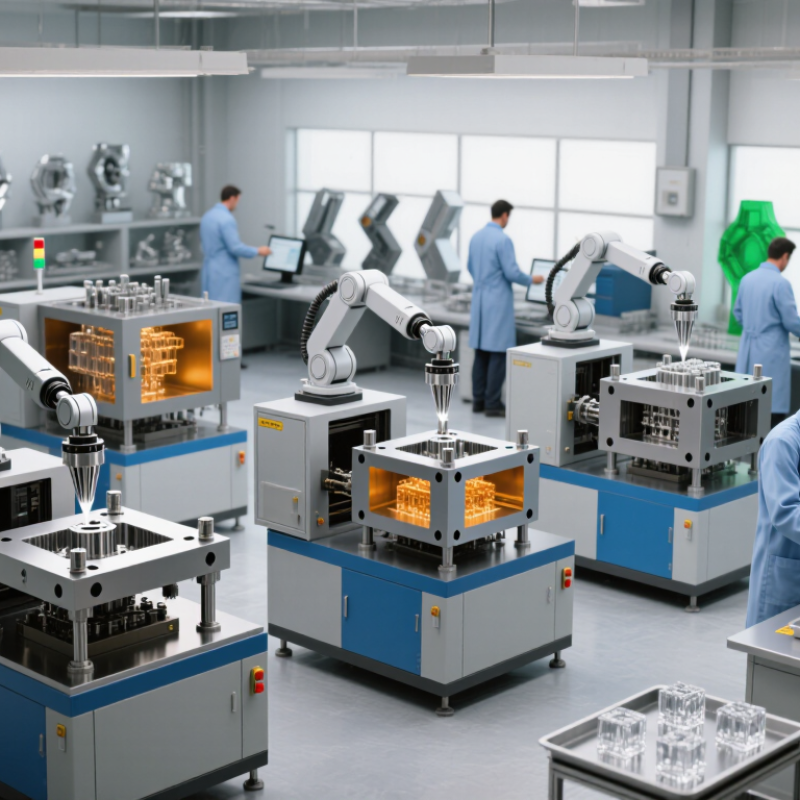
Prototype molding turns a digital design into a physical part for testing, fitting, and customer feedback. Injection molding uses a mold, heated resin, pressure, and controlled cooling. This process exposes weak walls, sink marks, poor tolerances, and difficult assembly before mass production.
Manufacturers matter because their engineering choices affect both speed and evidence quality. A capable supplier can recommend draft angles, gate locations, resin grades, and realistic tolerances. According to the PlasticsEurope report Plastics—The Fast Facts 2023, global plastics production reached about 400.3 million tonnes in 2022. That scale shows why material selection and process control deserve serious attention. The Wohlers Report 2024 also recorded a 9.1% rise in global additive manufacturing revenues during 2023. This growth encourages hybrid workflows, where printed tools support early molding trials. However, a prototype is not a perfect forecast. A soft mold may behave differently from a hardened production tool. That assumption can fail.
Tips: Ask for a design-for-manufacturing review before quoting. Request sample measurements, resin certificates, and inspection photos. Compare cycle time, mold life, tolerance data, and revision support, not price alone. Keep a written record of every change.
A practical manufacturer should explain limitations clearly. It should also share evidence from similar materials and part geometries. “Fast” is useful only when the parts remain dimensionally reliable. Small details matter. A 0.2-millimeter mismatch can stop a snap-fit from closing. Careful prototype molding reduces uncertainty, but it cannot remove every production risk.
| Prototype Molding Method | Typical Materials | Tooling Approach | Typical Prototype Quantity | Typical Lead Time | Typical Dimensional Capability | Best-Fit Applications | Why Manufacturer Capability Matters |
|---|---|---|---|---|---|---|---|
| Prototype Injection Molding | Thermoplastics such as ABS, polypropylene, polycarbonate, nylon, POM, and TPU | Aluminum or soft-steel molds with simplified parting lines and inserts | Approximately 10 to 10,000 parts | About 2 to 6 weeks, depending on mold complexity and material availability | Commonly about ±0.05 to ±0.20 mm for controlled features; material shrinkage must be considered | Functional engineering prototypes, fit checks, product testing, and low-volume production | Tool design, mold-flow knowledge, process control, and inspection capability strongly affect consistency and surface quality |
| Vacuum Casting | Polyurethane resins that simulate ABS, polypropylene, rubber, nylon, or transparent plastics | Silicone molds produced from a master pattern | Approximately 5 to 30 parts per silicone mold | About 1 to 3 weeks after the master pattern is approved | Commonly about ±0.15 to ±0.30 mm, depending on part size and geometry | Appearance models, ergonomic studies, display samples, and small batches of complex parts | Pattern finishing, silicone selection, degassing, and resin mixing determine replication accuracy and cosmetic quality |
| Compression Molding | Thermosets, elastomers, silicone compounds, rubber, and fiber-reinforced compounds | Machined or cast compression tooling with heated platens | Approximately 10 to 5,000 parts | About 2 to 6 weeks | Commonly about ±0.10 to ±0.50 mm, depending on material and part geometry | Seals, gaskets, covers, electrical insulation, and heat-resistant components | Compound formulation, curing control, flash management, and mold venting are important for repeatable results |
| Liquid Silicone Rubber Molding | Liquid silicone rubber in different hardness grades, colors, and specialty formulations | Precision metal mold with cold-runner or conventional injection tooling | Approximately 50 to 10,000 parts | About 3 to 8 weeks, including mold fabrication and validation | Commonly about ±0.10 to ±0.30 mm, with allowances for silicone elasticity and shrinkage | Medical covers, seals, keypads, wearable components, and flexible consumer products | Clean-room practices, material traceability, flash control, and curing expertise are important for reliable silicone parts |
| Rotational Molding | Polyethylene, polypropylene, nylon, PVC, and other rotational-molding powders | Fabricated sheet-metal or cast-metal molds rotated inside a heated chamber | Approximately 10 to 1,000 parts | About 3 to 8 weeks | Commonly about ±0.50 to ±1.50 mm; wall thickness and warpage require design allowance | Large hollow enclosures, tanks, containers, ducts, and durable outdoor products | Heating-cycle control, powder distribution, vent design, and cooling practices influence wall uniformity and distortion |
| Reaction Injection Molding | Polyurethane, structural polyurethane, and other two-component thermoset systems | Machined or cast molds with controlled mixing and metering equipment | Approximately 10 to 5,000 parts | About 3 to 8 weeks | Commonly about ±0.20 to ±0.60 mm, depending on material, mold, and part size | Large panels, automotive-style components, housings, and lightweight structural parts | Accurate chemical metering, mold temperature control, venting, and operator expertise affect density and mechanical performance |
| Low-Pressure Reaction Molding | Polyurethane foams, rigid polyurethane, and elastomeric polyurethane systems | Lower-pressure molds made from aluminum, epoxy, or composite tooling | Approximately 5 to 1,000 parts | About 2 to 6 weeks | Commonly about ±0.30 to ±1.00 mm, depending on foam density and part dimensions | Interior panels, protective packaging, soft-touch components, and low-volume enclosures | Control of foam density, expansion, skin formation, and dimensional stability determines final part performance |
| Bridge Tooling for Low-Volume Production | Production-grade thermoplastics, elastomers, and selected engineering resins | Short-life aluminum or soft-steel mold used before full production tooling | Approximately 100 to 20,000 parts | About 4 to 10 weeks | Commonly about ±0.05 to ±0.25 mm for controlled features | Market testing, pilot production, regulatory samples, and early customer shipments | Engineering validation, mold durability, quality documentation, and scalable process settings reduce transition risk |
© 2024 Sierramotion. All Rights Reserved