Call Today: 916-259-1868

Top 10 Copper Part Machining Manufacturers Worldwide

Choosing a reliable supplier for Copper Part Machining requires more than comparing website claims. Electrical conductivity, thermal performance, corrosion resistance, and dimensional stability all influence the final result. A suitable manufacturer must control these details from material selection through inspection.

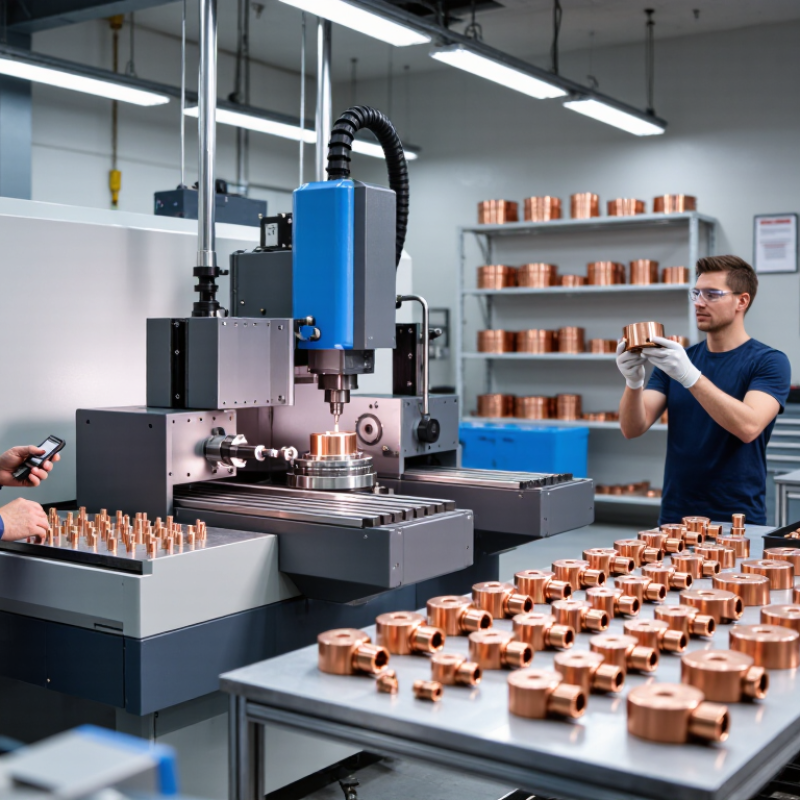
This guide examines ten leading Copper Part Machining manufacturers worldwide. It considers machining capability, copper alloy experience, production capacity, tolerance control, surface finishing, and quality documentation. Practical indicators matter. These include calibrated CMM equipment, traceable material certificates, clear sampling procedures, and responsive engineering support. A workshop producing tiny connectors may not suit large cooling plates. The reverse can also be true.

Real manufacturing experience often reveals what brochures omit. Tool wear, burr formation, heat buildup, and copper’s softness can affect consistency during production. Strong manufacturers address these issues through suitable tooling, controlled cutting parameters, and frequent in-process checks. Their teams should also understand drawings, GD&T requirements, and prototype-to-volume transitions.

This list is not absolute. Supplier performance can change with equipment, staffing, workload, or project complexity. That deserves attention. Rankings may also reflect available public information rather than every private capability. Buyers should request current samples, inspection reports, lead-time commitments, and references before placing substantial orders. A careful review can prevent costly rework, delayed assemblies, and inconsistent electrical performance. The best partner is not always the largest one. It is the manufacturer that consistently matches technical requirements, communication expectations, and production risk.
Top 10 Copper Part Machining Manufacturers Worldwide

Copper Part Machining: Definition, Scope, and Industrial Applications

Copper part machining is the controlled removal of material from copper or copper alloys. It creates precise components through turning, milling, drilling, and threading. These methods support both simple fittings and complex electrical parts.

The scope covers pure copper, brass, bronze, and specialized high-conductivity alloys. Engineers select each material according to conductivity, strength, corrosion resistance, and heat transfer needs.

Copper conducts heat rapidly, which can complicate cutting. Heat builds quickly. Sharp tools, stable fixturing, and suitable cutting fluids help reduce burrs and deformation.

However, these controls are not universal. A setting that works for brass may damage soft copper.

Industrial applications include electrical connectors, busbars, grounding components, heat exchanger plates, sensor housings, and precision plumbing parts. In production, machinists check thread quality, surface finish, hole position, and dimensional stability. Coordinate measuring machines and optical inspection systems can verify critical features.

Experienced teams also inspect tool wear during the run, not only after it ends. This practice improves consistency but increases inspection time.

A drawing may appear complete while omitting edge-break details or clamping limits. Careful communication is still essential. Reliable machining depends on material certificates, calibrated equipment, documented inspection records, and practical feedback from the shop floor.
Criteria for Evaluating Global Copper Machining Manufacturers

Evaluating the top copper part machining manufacturers requires more than comparing equipment lists. Real production experience matters. A capable supplier should explain how it controls burrs, heat, tool wear, and surface oxidation during machining. Ask for samples made from relevant grades, such as C101 or C110 copper. Inspect their dimensional reports, surface finishes, and edge quality.

Technical evidence should support every claim. Review calibration records, inspection methods, material certificates, and traceability procedures. Coordinate measuring machines, optical systems, and statistical process control can reveal process stability. However, expensive equipment does not guarantee reliable parts. No scorecard is perfect. A factory may show excellent prototypes but struggle with repeat orders, tight tolerances, or changing volumes.

Communication is another practical measure. Engineers should respond clearly to drawings, tolerance risks, and manufacturability concerns. Request a documented first-article process and ask how nonconforming parts are handled. Delivery history, capacity planning, and transparent corrective actions also indicate operational maturity. During an audit, observe chip control, coolant management, housekeeping, and operator training. Small details often expose larger weaknesses. A supplier that admits limitations may be more dependable than one offering effortless perfection. Checking independent customer references and recent performance data adds useful confidence before long-term production begins.

Top 10 Copper Part Machining Manufacturers Worldwide — Criteria for Evaluating Global Copper Machining Manufacturers

This evaluation framework uses practical procurement criteria for copper machining suppliers. The weighting reflects the relative importance of precision, copper-specific process expertise, quality control, production capacity, delivery performance, certification, and sustainability when comparing global manufacturers.

The percentages represent an objective supplier-screening model rather than the performance of any specific company. Copper-specific evaluation should also verify material traceability, electrical conductivity requirements, tolerance capability, surface-finish control, inspection records, and compliance with applicable ISO and customer standards.

Machining Technologies Used for Precision Copper Components

Top 10 Copper Part Machining Manufacturers Worldwide

Precision copper components demand more than standard CNC settings. Copper carries heat and electricity quickly, so cutting conditions can change during production. Heat moves quickly. Excessive tool pressure may create burrs, smeared edges, or dimensional drift.

Experienced manufacturers commonly use CNC milling, turning, and Swiss-type machining for small, detailed parts. Carbide tools help maintain edge stability, while sharp geometries reduce material deformation. Electrical discharge machining can produce narrow slots and complex profiles when conventional cutting becomes difficult. Controlled coolant flow is equally important. It removes heat, clears chips, and protects surface quality around deep pockets.

Quality control begins with a stable process, not only final inspection. Coordinate measuring machines verify hole locations, diameters, and flatness. Optical systems can check tiny edges without applying contact pressure. For electrical components, manufacturers may also test conductivity, plating thickness, and contact resistance. Surface roughness measurements reveal problems that visual inspection often misses.

Small errors matter. A drawing may specify tight tolerances, yet material condition and clamping force can still affect results. That assumption can fail. Careful suppliers record tool life, spindle loads, coolant conditions, and inspection data across batches. In practice, no process is perfect. A reliable manufacturer reviews failed or borderline parts, adjusts the method, and documents why the change was made. This disciplined feedback improves repeatability for connectors, heat sinks, terminals, and other precision copper components.

Profiles of the Top 10 Copper Part Machining Manufacturers Worldwide

The leading copper part machining manufacturers worldwide differ in equipment, specialization, and production scale. One supplier focuses on high-speed CNC milling for electrical connectors, using controlled feeds to prevent burrs. Another serves plumbing applications, where clean threads and leak-resistant surfaces matter. A third combines Swiss-type turning with automated bar loading for small, repetitive components. Its inspection records often include diameter checks measured in microns.

A fourth manufacturer supports heat-transfer equipment with deep-hole drilling and careful chip evacuation. A fifth produces custom copper busbars, adding bending and deburring after machining. The sixth specializes in prototype work, helping engineers test revised designs before larger production runs. The seventh operates large horizontal machining centers for heavier copper assemblies. It must manage heat carefully. Copper conducts heat quickly, yet it can smear when cutting conditions are poorly chosen.

The eighth supplier emphasizes medical and laboratory components, where traceability and surface cleanliness receive close attention. A ninth focuses on export production, coordinating material certificates, packaging, and dimensional reports across regions. The tenth combines machining with laser marking and final assembly, reducing handling between operations. Experienced buyers should examine tool life, inspection methods, tolerance history, and response times rather than relying on impressive equipment lists. No manufacturer performs perfectly on every copper grade. Some may also underestimate distortion after machining. That weakness deserves honest discussion before approval.

Comparing Capabilities, Quality Standards, and Market Coverage

A practical review of ten leading copper part machining manufacturers should examine more than equipment lists. Their capabilities differ across CNC turning, five-axis milling, Swiss machining, and wire EDM. Copper alloys also matter. Pure copper conducts heat well, while brass and bronze often machine more easily. Experienced manufacturers confirm the alloy, temper, drawing revision, and surface requirements before quoting.

Quality depends on repeatable control. Strong suppliers commonly operate under ISO 9001 systems and use calibrated CMMs, optical comparators, and in-process inspection. For demanding sectors, traceability, material certificates, first-article inspection, and documented corrective actions provide useful evidence. A tolerance of ±0.01 mm may be realistic for one feature, but not for every surface on a complex part. That detail is often overlooked. Scrutinize the inspection plan.

Market coverage reveals another difference. Some manufacturers support customers across North America, Europe, and Asia through regional warehouses or technical teams. Others rely mainly on export agents, which may slow engineering changes and after-sales communication. Compare export experience, packaging methods, lead-time stability, and customs documentation. A reliable supplier should explain capacity during peak periods, not only quote an attractive unit price. Public information can be incomplete, so an audit, sample order, and video inspection remain valuable. No manufacturer is strongest everywhere. Availability, communication, and process discipline may matter as much as advanced machinery.

Top 10 Copper Part Machining Manufacturers Worldwide - Comparing Capabilities, Quality Standards, and Market Coverage
Rank Manufacturer Profile Primary Operating Region Core Copper Machining Processes Typical Copper Materials Typical Precision Capability Quality and Compliance Standards Production Scale Key End Markets Market Coverage Overall Capability Score
1 Profile A North America High-speed CNC turning, 3-, 4-, and 5-axis milling, Swiss-type machining, deep-hole drilling C10100, C11000, C12200, C14500, copper alloys and brass Typical dimensional tolerance: ±0.005 mm; production surface finish down to Ra 0.8 µm ISO 9001; AS9100-based aerospace quality systems; material traceability and first-article inspection Prototype to high-volume production; automated pallet and bar-feed systems Aerospace, electrical distribution, defense, medical equipment North America, Europe, and Asia-Pacific through export supply chains 9.5 / 10
2 Profile B Western Europe Multi-axis CNC milling, precision turning, thread machining, micro-drilling, deburring and cleaning Electrolytic tough-pitch copper, oxygen-free copper, tellurium copper, brass and bronze Typical dimensional tolerance: ±0.010 mm; surface finish commonly Ra 1.6 µm or better ISO 9001; ISO 14001; documented calibration, inspection planning and batch traceability Low- to medium-volume precision production with strong engineering support Industrial automation, power electronics, rail, energy systems European Union, United Kingdom, Middle East, and selected Asian markets 9.3 / 10
3 Profile C East Asia High-volume CNC turning, multi-spindle machining, milling, tapping, broaching and in-process inspection C11000, C10200, C14500, free-machining copper alloys and brass Typical dimensional tolerance: ±0.010–0.020 mm; repeatability supported by automated gauging ISO 9001; IATF 16949-oriented automotive controls; PPAP and statistical process control capability High-volume production; dedicated cells for repeat copper components Automotive, charging equipment, connectors, motors and household appliances Asia-Pacific, North America, Europe, and global contract manufacturing networks 9.1 / 10
4 Profile D Central Europe Precision CNC turning, 5-axis milling, electrical discharge machining, laser marking and assembly Pure copper, oxygen-free copper, brass, bronze and nickel-copper alloys Typical dimensional tolerance: ±0.010 mm; form and position inspection using CMM equipment ISO 9001; ISO 13485 for applicable medical production; controlled clean-process documentation Prototype, pilot and medium-volume production Medical devices, laboratory equipment, semiconductor tooling, industrial electronics Europe, North America, and selected Asia-Pacific customers 8.9 / 10
5 Profile E East Asia CNC turning, 3- and 5-axis milling, skiving, slotting, heat-treatment coordination and surface finishing C11000, C10200, C17200, brass, phosphor bronze and copper-nickel alloys Typical dimensional tolerance: ±0.015 mm; fine features and small-batch repeatability available ISO 9001; ISO 14001; RoHS and REACH material-compliance documentation Prototype to medium and high-volume production Telecommunications, electronics, renewable energy, industrial controls Asia-Pacific, Europe, North America, and Southeast Asia 8.7 / 10
6 Profile F North America CNC turning, vertical and horizontal milling, mill-turn machining, thread milling and assembly C10100, C11000, C12200, brass, bronze and copper-nickel alloys Typical dimensional tolerance: ±0.015 mm; inspection supported by CMM and optical measurement ISO 9001; NADCAP-accredited special processes available through qualified partners; full lot records Prototype, low- and medium-volume production Defense, aerospace, marine systems, power generation United States, Canada, Europe, and approved defense supply chains 8.6 / 10
7 Profile G South Asia CNC turning, milling, drilling, tapping, gear-related machining and secondary finishing C11000, C12200, free-machining copper, brass and bronze Typical dimensional tolerance: ±0.020 mm; tighter tolerances available on selected features ISO 9001; inspection reports, material certificates and export packaging controls Low- to high-volume production with competitive batch pricing Plumbing components, electrical hardware, pumps, industrial machinery South Asia, Europe, North America, and the Middle East 8.3 / 10
8 Profile H Southern Europe Swiss CNC machining, precision turning, milling, knurling, deburring and parts washing Electrolytic copper, tellurium copper, brass, bronze and copper-aluminum alloys Typical dimensional tolerance: ±0.020 mm; small-diameter parts down to approximately 1 mm are feasible ISO 9001; ISO 14001; documented sampling plans and supplier material verification High-volume small-part production Automotive sensors, electrical terminals, instrumentation, HVAC equipment Europe, North Africa, and selected North American markets 8.1 / 10
9 Profile I East Asia Rapid CNC prototyping, 3- and 5-axis milling, turning, engraving and finishing coordination C10100, C11000, C12200, brass, bronze and copper-chromium alloys Typical dimensional tolerance: ±0.020–0.050 mm depending on geometry and batch size ISO 9001; digital inspection reports; material certificates and restricted-substance declarations Rapid prototypes, engineering samples and short-run production Consumer electronics, robotics, product development, research equipment Worldwide online and export fulfillment coverage 7.9 / 10
10 Profile J Eastern Europe CNC turning, milling, drilling, tapping, broaching and mechanical subassembly C11000, C12200, brass, bronze and copper-nickel alloys Typical dimensional tolerance: ±0.025 mm; inspection based on drawing requirements and sampling plans ISO 9001; ISO 14001; traceable inspection records and supplier quality controls Prototype to medium-volume production Industrial equipment, electrical enclosures, heating systems, general engineering European Union, United Kingdom, Turkey, and nearby export markets 7.7 / 10

Data note: Capability ranges represent commonly published or industry-standard values for comparable copper machining operations. Actual tolerances, surface finishes, certifications, material grades, production volumes, and export coverage should be confirmed directly against current supplier documentation and part-specific drawings.