How to Choose the Right Aluminum Die Cast Mold?
Choosing the right Aluminum Die Cast Mold is a production decision, not merely a tooling purchase. The choice affects cycle time, part quality, maintenance, and total cost. Grand View Research and Fortune Business Insights both report strong growth across the global die casting market, driven largely by automotive, electric vehicle, and industrial applications. Their findings point toward higher output and tighter dimensional requirements. That pressure makes mold design increasingly important.
Dr. Steve Midson, a recognized aluminum casting specialist, offers a useful principle: “Good casting begins with controlling the process, not correcting defects afterward.” The quotation captures a practical truth. Mold selection should begin with the alloy, wall thickness, projected area, annual volume, and expected shot count. H13 tool steel may suit demanding thermal cycles, but steel grade alone does not guarantee long service life. Cooling channels, venting, gate design, surface treatment, and ejection layout matter just as much.
Small details matter.
A mold that looks economical may create flash, soldering, or premature heat checking. A complex cooling system may improve stability, yet raise manufacturing and repair costs. Industry reports provide valuable market direction, but they cannot replace trials using your actual alloy and machine. That is where experience becomes measurable. Review filling simulations, inspect early samples, and record thermal fatigue after repeated cycles. I would not claim one universal mold formula exists. Real production conditions are often less tidy than design documents suggest. The right Aluminum Die Cast Mold balances performance, serviceability, risk, and realistic production evidence.
Define the Product Requirements and Performance Expectations
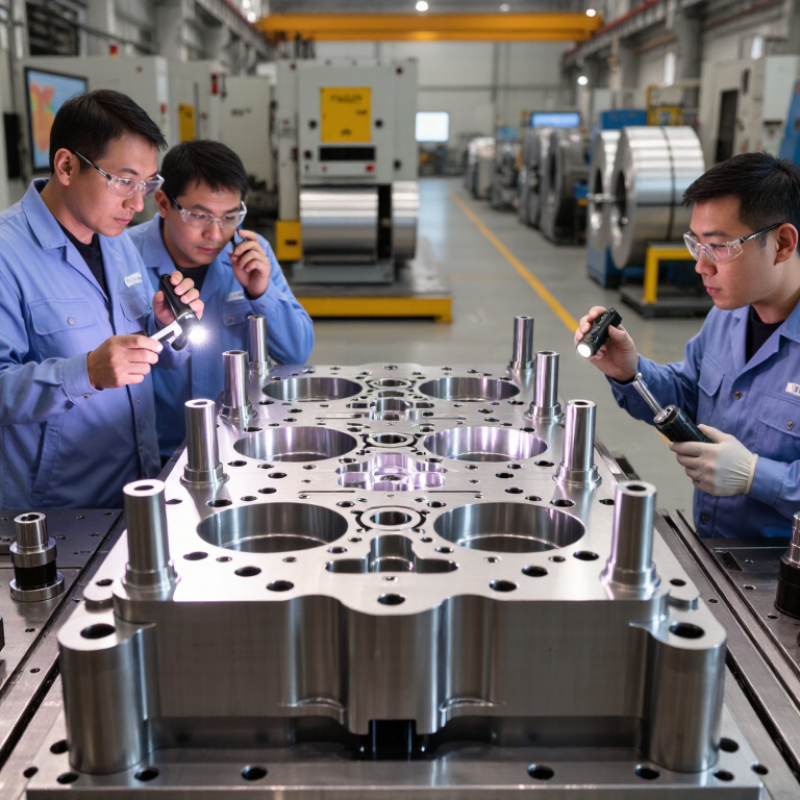
Choosing an aluminum die cast mold starts with defining the product, not selecting steel or cavity layouts. Record the part’s weight, wall thickness, projected area, alloy, surface finish, and annual volume. Clarify whether the component needs pressure tightness, electrical conductivity, wear resistance, or cosmetic quality. Small details matter.
The North American Die Casting Association recommends evaluating dimensional tolerances, draft, parting lines, and ejection requirements during product design. A tight tolerance may require better process control and more expensive mold construction. It may also increase inspection time. The U.S. Department of Energy identifies material efficiency and reduced scrap as important opportunities in metal casting. Therefore, set an acceptable scrap rate before requesting mold quotations. A 1% target may be unrealistic for a complex, thin-walled housing.
Production expectations must include cycle time, mold life, maintenance access, and expected repair intervals. The International Aluminium Institute projects strong growth in aluminum demand through 2030, increasing pressure for stable and efficient casting capacity. Ask whether the mold can support that workload, not merely complete initial samples. Define cooling performance with measurable limits, such as temperature balance across critical cavities. Include evidence from similar tooling trials, inspection records, and thermal studies. Experience suggests that suppliers often promise longer mold life than actual factory conditions deliver. Treat those promises as estimates, not guarantees. A practical specification leaves room for revision.
Select the Appropriate Aluminum Die Casting Mold Material
How to Choose the Right Aluminum Die Cast Mold?
Choosing the right mold material starts with heat, pressure, and expected production volume. For aluminum die casting, H13 hot-work tool steel remains a practical baseline. ASM Handbook, Volume 1, reports H13 thermal conductivity near 24–28 W/m·K at room temperature. This helps move heat away from the cavity surface. Faster heat removal can reduce soldering and thermal shock. However, conductivity alone cannot determine mold life.
NADCA’s 2023 Product Specification Standards highlight thermal fatigue, dimensional control, and surface quality as critical die-casting factors. Thermal fatigue often limits service life before simple wear does. For long production runs, nitrided H13 may improve surface hardness and resistance to aluminum adhesion. Some engineers choose harder steel too early. That choice can backfire. Excessive hardness may reduce toughness and increase cracking around sharp corners, slides, or thin ribs. A small fillet can matter more than a higher hardness value.
Material selection should also consider repair and sustainability. The International Aluminium Institute reports that recycled aluminum typically requires about 5% of the energy used for primary aluminum production. A mold that survives more cycles can support lower material waste and fewer replacements. Yet this benefit depends on maintenance, cooling design, and correct heat treatment. In practical trials, record cavity temperature, shot count, crack locations, and polishing intervals. The data may challenge the original material choice.
Evaluate Mold Design, Structure, and Manufacturing Accuracy
Choosing the right aluminum die cast mold begins with its design, not its price. A reliable design matches the alloy, part geometry, wall thickness, and production volume. Examine draft angles, parting lines, runners, gates, and overflow wells. These details control filling, air removal, and trimming. Sharp corners often create stress and premature cracking. Smooth transitions are safer.
Mold structure must withstand repeated clamping and thermal cycling. Inspect the base, inserts, slides, ejector pins, cooling channels, and guide components. A balanced cooling layout reduces distortion and cycle variation. Keep cooling channels away from thin steel sections. Otherwise, heat may weaken the mold. Service access also matters. Technicians should reach wear parts without dismantling the entire tool. Convenient maintenance can save hours.
Manufacturing accuracy requires more than one attractive sample. Verify cavity dimensions, alignment, surface finish, and insert matching through drawings and coordinate measurements. Small parting-line errors can create flash. Uneven ejector movement may leave marks or deformation. Request inspection records, material certificates, and process controls. Measure several shots after the mold reaches working temperature. This reveals thermal movement and repeatability. I have seen excellent first samples hide unstable production conditions. That mistake is easy to make. A precise mold can still perform poorly with unsuitable pressure or cooling. Clear measurements and realistic trials matter.
How to Choose the Right Aluminum Die Cast Mold?
Evaluate mold design, structure, and manufacturing accuracy using practical dimensional-control checkpoints. Lower deviation values indicate tighter mold accuracy requirements.
Typical engineering reference limits vary by part size, alloy, tooling method, and required casting tolerance.
Compare Mold Cooling, Ejection, and Maintenance Features
How to Choose the Right Aluminum Die Cast Mold?
Cooling, ejection, and maintenance features directly affect mold life and casting consistency. In production, I inspect cooling channels before reviewing cosmetic details. Channels should run close to thick sections without creating weak areas in the mold steel. Balanced water flow helps control shrinkage, soldering, and cycle time. Simple access matters too. Blocked passages can turn a routine service into a long shutdown.
I once selected a mold with excellent cooling performance but limited ejector access. That assumption was wrong. Technicians needed extra time to remove pins and inspect hidden wear. A better mold includes replaceable ejector pins, guided plates, and clear inspection points. Ejection force should spread evenly across the casting. Otherwise, thin ribs may bend or leave marks. Ask for practical service drawings, not only polished specifications.
Maintenance design deserves careful attention. Removable inserts, accessible fasteners, and standard lubrication points reduce repair delays. Drain ports can prevent trapped water from causing corrosion during storage. Keep records of cycle counts, vent cleaning, and dimensional checks. Small evidence helps identify gradual damage. Still, maintenance plans are not perfect. Dust, operator habits, and alloy temperature can change the results. Test the mold under realistic conditions before approving full production.